
HDPE Pipe Fusion Machine for South American Mining Contractors: How to Select a Supplier
Table of Contents
This guide explains how South American mining contractors can select an HDPE pipe fusion machine supplier. It covers machine types, high-altitude specifications, standards, data logging, spare parts, lead time, and total landed cost to help reduce project risk.
What Is an HDPE Pipe Fusion Machine and Which Types Do Mining Projects Use?
An HDPE pipe fusion machine joins polyethylene pipes by heating their ends to a molten state, usually between 200°C and 230°C. Once the plastic softens, the machine presses the surfaces together using precise hydraulic pressure. What happens next? The two pieces cool into a single, leak-proof joint. This monolithic bond easily handles the extreme pressures and highly abrasive materials common in heavy industrial and mining operations.
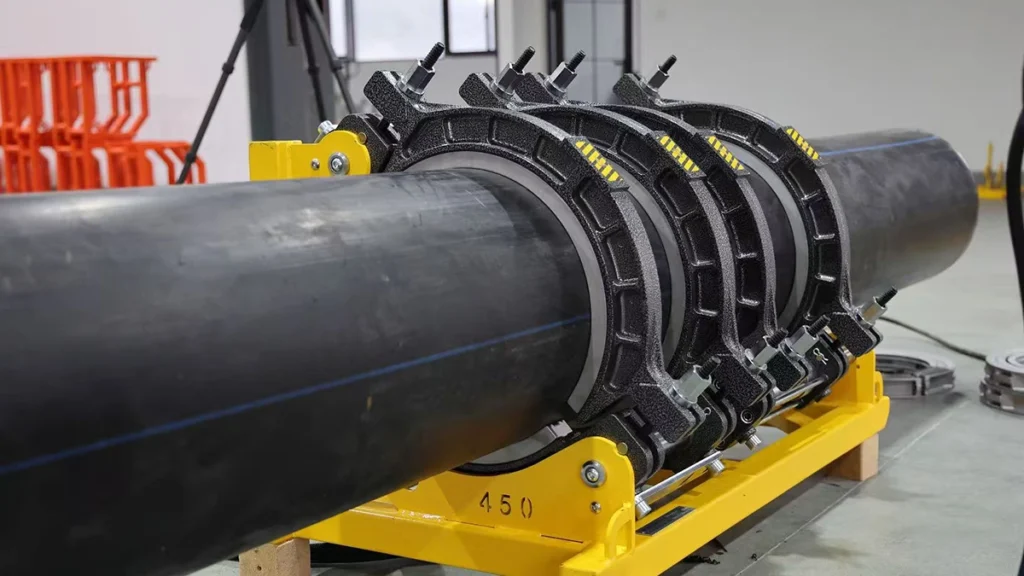
HDPE Pipe Fusion Machine: A Short Definition
Fundamentally, an HDPE pipe fusion machine acts as a specialized thermal welder built specifically for thermoplastic piping. It manages three critical variables: temperature, heating time, and hydraulic clamping force. When an operator dials these settings in correctly, the butt fusion welding machine seamlessly bonds two pipe ends. A properly executed fusion joint doesn’t just hold the pipe together—it actually becomes as strong as, if not stronger than, the original pipe wall.
Hydraulic Butt Fusion vs Electrofusion vs Workshop Fabrication Machines
Mining contractors don’t use a one-size-fits-all approach. They select fusion equipment based on pipeline location, pipe diameter, and the specific geometry of the joint. Knowing the differences between these methods guarantees you bring the right tool to the job site.
| Fusion Method | Typical Diameter Range | Typical Mining Use | Field Portability | Key Limitation |
|---|---|---|---|---|
| Hydraulic Butt Fusion | 160mm – 2000mm+ | Main slurry lines, tailings, process water | High (wheeled or track-mounted) | Requires space for machine footprint |
| Electrofusion | 20mm – 800mm | Tie-ins, repairs, tight-space installations | Very High (small control box) | High cost per fitting; strict scraping needs |
| Workshop Fabrication | 315mm – 1200mm | Off-site manufacturing of tees and elbows | None (stationary CNC machine) | Cannot be used for field pipeline assembly |
Which Fusion Method Is Standard for Large-Diameter Mining Pipelines?
For large-diameter mining HDPE pipelines, hydraulic butt fusion stands as the undisputed industry standard. It delivers unmatched joint strength and sealing reliability. That performance is absolutely vital when pumping abrasive slurries through thick-wall SDR pipes. Electrofusion, on the other hand, usually steps in for tricky tie-ins, emergency fixes, or tight trenches where a massive hydraulic carriage simply won’t fit.
Why Supplier Choice Is Critical for South American Mining Contractors
Picking the right supplier for your HDPE pipe fusion machine isn’t just a procurement detail in South America—it makes or breaks a project. Mining operations here battle punishing altitudes, wild temperature swings, and uncompromising quality control demands. If your equipment fails up in the mountains, you aren’t just looking at delayed schedules. Contractors face crushing financial penalties and massive operational headaches.
High Altitude, Dust, and Temperature Swings in the Andes
Picture a mining site in Chile or Peru. Crews routinely work at elevations pushing 3,000 to 4,000 meters. These brutal environments demand a hydraulic butt fusion machine tailored for high-altitude mining, complete with dust-proof enclosures and heavy-duty hydraulic seals. Add sudden ambient temperature drops to the mix, and you suddenly need highly stable heating plates. The equipment must instantly compensate for heat loss to meet strict ISO 21307 butt fusion machine requirements.
What Does a Failed Fusion Joint Cost on a Mining Pipeline?
A single botched DN400 joint can hit a contractor with an estimated $15,000 bill. That painful number covers the labor to dig up the site, the ruined materials, and the specialized team brought in to cut out and re-weld the bad section. Worse still, that $15,000 doesn’t even factor in the catastrophic expense of operational downtime or the environmental nightmare of a tailings spill.
Mine-Owner QA/QC and Weld Traceability Expectations
Tier 1 mining giants like Codelco and BHP refuse to compromise on weld traceability. Gone are the days of relying on handwritten logbooks. Today’s HDPE pipe fusion machines must meet ISO 12176-4 standards, using barcode scanners to lock in operator badge IDs, pipe batch numbers, and exact GPS coordinates. This digital paper trail ensures every single weld passes the mine owner’s rigorous QA/QC audits.
Factory-direct pricing with technical consultation included
Get Your Free QuoteMining Applications and Their Fusion Machine Requirements
Different mining applications demand totally different fusion setups. Slurry and tailings lines require high-pressure butt fusion welding machines capable of wrangling thick-walled pipes. Meanwhile, dewatering systems and process water networks prioritize speed and mobility. Project efficiency hinges on matching the right HDPE pipe welding machine class to your specific pipe diameter and SDR rating.
Tailings and Slurry Lines: Large Diameter and Thick-Wall SDR Pipes
Moving highly abrasive tailings requires serious hardware, typically thick-wall pipes like SDR 7.4 or SDR 9. An HDPE pipe fusion machine tasked with tailings pipelines has to generate massive hydraulic clamping force. Why? It must physically overcome the heavy drag pressure of these massive pipes. If the hydraulic cylinders are weak, they simply won’t hit the required interfacial pressure during the crucial bead-up phase.
Process Water, Dewatering, and Heap Leach Solution Lines
Unlike massive, stationary tailings lines, heap leach irrigation and process water systems usually run mid-range diameters (160mm to 315mm). These jobs require highly mobile butt fusion welding machines. Crews need wheeled or track-mounted units they can drag rapidly across the site to keep up with punishing installation schedules.
Which Machine Size Range Does a Typical Copper or Gold Mine Project Need?
A standard mining fleet rarely relies on just one HDPE pipe fusion machine. Contractors need a diverse mix of sizes to juggle multiple pipeline packages at once.
| Application | Typical OD Range | Typical SDR | Recommended Machine Class | Special Notes |
|---|---|---|---|---|
| Process Water | 160mm – 315mm | SDR 11 – 17 | 315mm Wheeled/Manual | High mobility required for fast progression |
| Standard Slurry | 315mm – 630mm | SDR 9 – 11 | 630mm Hydraulic CNC | Requires robust facer motor for thick walls |
| Main Tailings | 800mm – 1200mm+ | SDR 7.4 – 9 | 1200mm Heavy-Duty Hydraulic | Needs crane assist and high drag capacity |
| Heap Leach Lines | 110mm – 250mm | SDR 11 – 17 | 250mm Manual/Semi-Auto | Frequent moves across uneven leach pads |
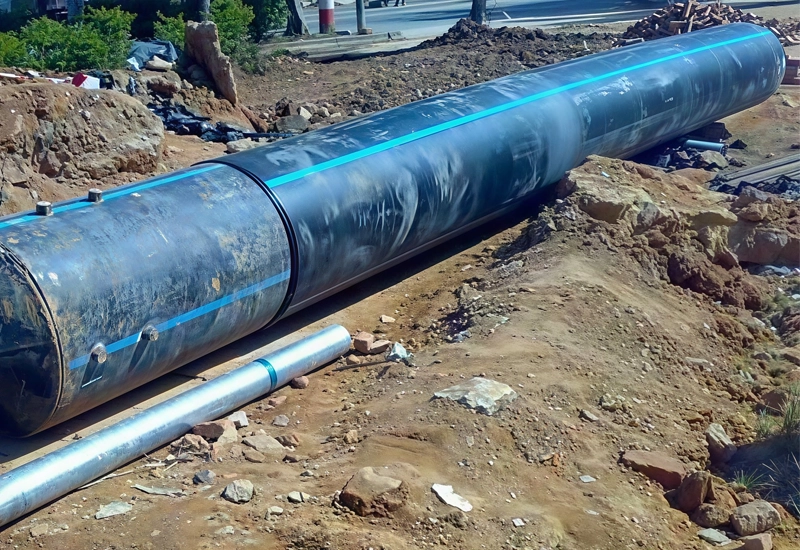
Scenario: Contractor Running Multiple Pipeline Packages on One Site
Imagine managing several pipeline packages simultaneously. You have to optimize your equipment fleet so expensive machinery doesn’t sit idle. By partnering with a top-tier large diameter HDPE pipe fusion machine supplier, contractors can source versatile equipment that uses reduction inserts. Take a 630mm butt fusion machine, for instance. Drop in the right inserts, and you can seamlessly weld 315mm, 355mm, 400mm, 450mm, and 500mm pipes, squeezing maximum value out of a single asset.
Technical Specifications to Verify Before Shortlisting a Supplier
Procurement teams need to nail down exact technical specifications before they even think about shortlisting a supplier. You have to look hard at the diameter range, hydraulic pressure capacity, power supply needs, and how well the heater plate holds its temperature. Verifying compliance with international standards guarantees the butt fusion welding machine won’t choke when faced with brutal site conditions.
Diameter Range, SDR Capability, and Hydraulic Pressure
The HDPE pipe welder’s hydraulic cylinders must hit the necessary Interfacial Pressure (IFP) required for thick-walled pipes. Smart procurement teams rely on a structured checklist to confirm these heavy-duty technical parameters.
| Parameter | What to Verify | Why It Matters for Mining | Question to Ask the Supplier |
|---|---|---|---|
| Diameter & SDR | Max OD and max wall thickness | Thick SDR 7.4 pipes require heavy clamping force. | Can the cylinders overcome the drag pressure of a 12m SDR 7.4 pipe? |
| Hydraulic Pressure | Gauge accuracy and max bar/MPa | Ensures compliance with high-pressure standards. | Does the hydraulic unit maintain pressure without bleed-off during the soak phase? |
| Heater Plate | Temperature uniformity across the plate | Cold spots lead to brittle, failed welds. | What is the maximum temperature deviation across the heating surface? |
| Facer Motor | kW rating and torque | Underpowered facers stall on thick HDPE walls. | Is the facer motor rated for continuous heavy-duty shaving? |
| Power Supply | Voltage and frequency compatibility | South American sites vary between 50Hz and 60Hz. | Can the machine be configured for 380V 3-phase at 50Hz? |
Heater Plate Temperature Stability and Coating Quality
Your heater plate needs to hold a rock-steady temperature between 200°C and 240°C. See a temperature swing greater than 15°C? That’s a huge red flag pointing to a failing heating element or a loose thermocouple. Furthermore, a premium PTFE (Teflon) coating isn’t a luxury—it’s mandatory. Without it, molten polyethylene sticks to the plate, completely ruining the joint.
Voltage, Frequency, and Generator Sizing for Remote and High-Altitude Sites
Running a hydraulic butt fusion machine for high altitude mining requires serious power planning. Larger diameter butt fusion machines (anything 450mm and up) absolutely require 380V three-phase power. Here’s the catch: once you climb past 3,000 meters, diesel generators suffer massive power derating. Contractors have to heavily oversize their industrial kVA generators. Otherwise, the massive amp draw from the hydraulic pump and heating plate will trip breakers all day long.
Which Standards Should the Machine Comply With (ISO 12176, ISO 21307, ASTM F2620, DVS 2207)?
Tender documents almost always demand strict adherence to global welding codes. Procurement teams must ask for hard proof of compliance with ISO 21307 butt fusion machine requirements, which dictates Single Low, Dual Low, and Single High-Pressure parameters. On top of that, ASTM F2620 lays out the American high-pressure rules (60-90 PSI), while DVS 2207-1 handles the German low-pressure parameters (21.75 PSI).
Why Does a Fusion Data Logger Matter for Mining Contracts?
Walking onto a Tier 1 mining project without an HDPE pipe welding machine with data logger capabilities is a recipe for rejection. It’s no longer optional. Data loggers capture the exact time, pressure, and temperature parameters for every single joint you weld. This creates a tamper-proof digital record proving the weld meets code, which makes handing the pipeline over to the mine owner’s QA/QC team infinitely smoother.
Get detailed specs and custom configuration options
Request Technical SpecificationsHow to Evaluate an HDPE Pipe Fusion Machine Supplier: Key Criteria
Sizing up an HDPE pipe fusion machine supplier means looking closely at their manufacturing muscle, quality control protocols, and regional service footprint. Procurement teams should demand factory test reports, check their mining project references, and rely on a strict scorecard to judge both commercial reliability and technical depth without bias.
Manufacturing Capability and Quality Control
When figuring out how to evaluate HDPE pipe fusion equipment manufacturers, buyers need to put the factory’s quality control under a microscope. Good suppliers run a documented Factory Acceptance Test (FAT) on every single unit. They use precision tools to verify clamp alignment accuracy and check the heating plate for perfectly uniform temperature distribution before they ever crate the butt fusion welding machine for shipping.
Certifications, Test Reports, and Mining Project References
A trustworthy supplier will readily hand over CE markings, ISO 9001 factory certifications, and compliance reports for ISO 12176-1 (which covers alignment and pressure accuracy). Beyond the paperwork, procurement teams should ask for reference projects specifically tied to mining. You need proof that their equipment actually survives harsh, dust-choked environments.
Does the Supplier Have Service Capacity in Chile, Peru, or Brazil?
Any HDPE pipe fusion machine supplier in South America needs to bring serious regional support to the table. Buyers should check if the manufacturer has local service hubs in key areas like Matarani, Antofagasta, or Santa Luzia. If they operate on a factory-direct model, they must prove they can expedite DHL parts dispatch and handle rapid export support to keep your downtime to an absolute minimum.
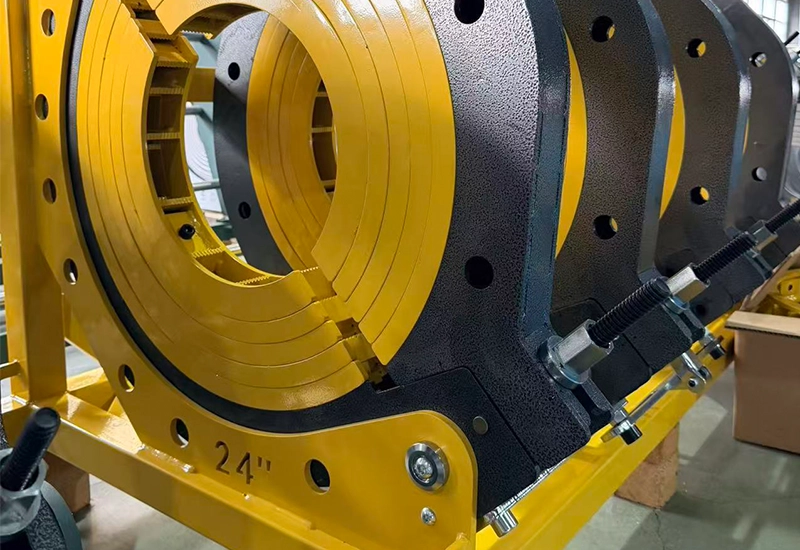
Supplier Evaluation Scorecard for Procurement Teams
Procurement teams should lean on a weighted scorecard to objectively compare quotes from any large diameter HDPE pipe fusion machine supplier.
| Criterion | Suggested Weight (%) | Evidence to Request | Red Flag |
|---|---|---|---|
| Technical Compliance | 30% | ISO 12176-1 test reports, data logger specs | Cannot support ASTM F2620 high pressure |
| Manufacturing QC | 20% | ISO 9001, documented FAT protocols | Refuses live video factory audit |
| Regional References | 15% | Case studies from LATAM mining projects | Only supplies to municipal water projects |
| Spare Parts & Service | 20% | Inventory list, remote support SLA | No critical spares package offered |
| Total Landed Cost | 15% | Transparent FOB/CIF pricing | Unclear warranty terms or hidden fees |
Manufacturer, Trading Company, or Local Distributor: Which Supplier Model Fits Your Project?
Contractors face a major choice when buying HDPE pipe fusion equipment: go direct to the manufacturer, use a trading company, or buy from a local distributor. Direct manufacturers offer deep technical customization and lower costs. Local distributors give you immediate regional support, but you’ll pay a premium for it. Often, a hybrid approach strikes the perfect balance for large-scale projects.
Direct Manufacturer: Pricing, Customization, and Technical Depth
As you learn how to evaluate HDPE pipe fusion equipment manufacturers, buying direct quickly stands out as a massive capital saver. Direct manufacturers provide custom voltage setups, specific data logger integrations, and drastically lower unit costs. The trade-off? The contractor has to shoulder the logistics of international ocean freight and import customs clearance.
Local Distributor: Faster Support but Higher Unit Cost
Local distributors offer the undeniable convenience of buying in local currency and having stock ready immediately. They take care of the import headaches and provide boots-on-the-ground technical support. Unsurprisingly, this convenience costs you. Distributors typically mark up equipment anywhere from 30% to 50% above the factory-direct price.
When Does a Hybrid Model (Manufacturer plus Local Service Partner) Make Sense?
For medium to large contractors, a hybrid model usually hits the sweet spot. You buy the heavy machinery directly from an overseas factory or an HDPE pipe fusion machine supplier in South America, saving a fortune on the initial fleet purchase. Then, you hire a local service partner purely for operator certification, periodic butt fusion welding machine calibration, and emergency spare parts.
Cost, Lead Time, and Logistics for Delivery to South America
The total landed cost of your fusion equipment isn’t just the sticker price. It includes the base butt fusion welding machine, spare parts, data loggers, ocean freight, and import duties. Getting equipment built and shipped to South American ports usually takes between 30 and 45 days. Contractors have to optimize their Incoterms and plan logistics proactively to prevent project delays.
What Drives the Price of an HDPE Pipe Fusion Machine?
Two main factors dictate the price of fusion equipment: the maximum diameter it can handle and its level of automation. A fully CNC automatic butt fusion machine naturally costs more than a semi-automatic model. Throw in heavy-duty hydraulic cylinders, advanced data loggers, and electric crane hoists for massive pipes, and your capital expenditure will rise accordingly.
Total Landed Cost: Freight, Duties, and Customs in Key Mining Countries
Smart contractors calculate the total landed cost, ignoring the illusion of the base factory price. This equipment normally imports under HS Code 85152900.
| Cost Component | What It Includes | Typical Share or Range | Notes |
|---|---|---|---|
| Base Machine | Chassis, clamps, facer, heater, hydraulics | 60% – 70% | Scales heavily with max diameter |
| Data Logger & CNC | Automation sensors and recording unit | 5% – 10% | Mandatory for most Tier 1 mine sites |
| Spare Parts Kit | First-aid maintenance components | 3% – 5% | Critical for remote site uptime |
| Ocean Freight | Shipping from origin port to LATAM | 10% – 15% | Varies by container size and global rates |
| Duties & Taxes | Import tariffs and local VAT | 5% – 20% | Often mitigated by bilateral trade agreements |
| Inland Transport | Trucking from port to remote mine site | 2% – 5% | Expensive for high-altitude deliveries |
Typical Production and Ocean Freight Lead Times to Callao, San Antonio, and Santos
Pinning down the HDPE pipe fusion machine price and lead time for Chile and Peru keeps your project schedule intact. Building large CNC automatic butt fusion machines usually takes 20 to 45 days. From major Asian manufacturing hubs, expect ocean freight transit times of 28 to 38 days to Callao (Peru), 32 to 42 days to Valparaíso or San Antonio (Chile), and roughly 35 to 45 days to Santos (Brazil).
Choosing Incoterms and Payment Terms to Reduce Procurement Risk
FOB (Free On Board) remains the go-to Incoterm. It requires the supplier to handle local logistics up to the departure port, freeing the buyer to control ocean freight via their trusted forwarder. CIF (Cost, Insurance, and Freight) flips the freight responsibility back to the supplier. For payments, T/T (Telegraphic Transfer) is standard practice, though an L/C (Letter of Credit) provides excellent security when ordering a massive multi-machine fleet.
After-Sales Service, Spare Parts, and Operator Training for Remote Mine Sites
You cannot maintain a remote pipeline construction schedule without rock-solid after-sales service and thorough operator training. Contractors need to lock in a critical spare parts package early and establish clear remote troubleshooting protocols. You don’t want a minor sensor fault shutting down your project for weeks.
Recommended Critical Spare Parts Package for a Mining Project
High-altitude sites don’t have the luxury of waiting weeks for replacement parts. Securing HDPE pipe fusion machine spare parts and after-sales support for mining contractors means buying a “first aid” kit on day one. This package should include replacement fuses and relays, a hydraulic seal kit (O-rings), at least two extra sets of planer blades, spare thermocouple sensors, and 5 to 10 liters of manufacturer-approved hydraulic oil.
How Fast Can a Supplier Respond to Breakdowns at a Remote Site?
If you don’t have spares on site, waiting for international parts can paralyze a pipeline project for 7 to 14 days, burning through thousands of dollars every single day. Suppliers must provide 24/7 remote troubleshooting via video call. A sharp technical team can usually walk site mechanics through replacing seals or bypassing a minor sensor fault, getting the butt fusion welding machine back up and running in hours instead of weeks.
Operator Training, Fusion Procedure Qualification, and Language Support
Training programs need to align with ISO 12176-3 or ASTM F3190 standards so operators fully grasp the bead-up, soak, and cooling phases. CNC machines loaded with multi-language interfaces—especially Portuguese and Spanish—cut training time from weeks down to days. These systems provide intuitive, on-screen prompts that walk local crews step-by-step through qualified fusion procedures.
Common Supplier Selection Mistakes and Hidden Risks
Picking an HDPE pipe fusion machine supplier based entirely on the lowest bid invites disaster. Contractors routinely make the mistake of ignoring altitude-related generator derating, forgetting to specify data loggers, or accepting generic safety certificates that completely fail to meet strict mining QA standards.
Choosing the Lowest Quote Without Verifying Fusion Pressure Accuracy
1. Mistake: Snapping up the cheapest HDPE pipe jointing machine without double-checking the quality of the hydraulic cylinders.
2. Consequence: Budget butt fusion welding machines inevitably suffer from hydraulic pressure bleed-off during the critical cooling phase. When this happens, you can’t maintain the strict interfacial pressure demanded by DVS 2207 or ASTM F2620. The result? Brittle, cold welds that snap under operational stress.
3. How to Avoid It: Insist on ISO 12176-1 compliance reports that prove the hydraulic unit can hold exact pressure over a long period without leaking a single drop.
Overlooking Power Supply and Generator Mismatch
1. Mistake: Assuming a massive 630mm hydraulic butt fusion machine can just plug into standard site power or run on a small generator.
2. Consequence: We see this scenario play out in northern Chile constantly. Contractors undersize their generators for high-altitude jobs. Because diesel generators lose massive efficiency above 3,000 meters, the butt fusion welding machine either refuses to heat up, or the hydraulic pump trips the breakers, bringing fusion work to a grinding halt.
3. How to Avoid It: Calculate the combined kW draw of the facer and heater, apply the manufacturer’s high-altitude derating formula, and bring in a heavily oversized 380V 3-phase generator.
Is a Generic CE Certificate Enough for Mining Tenders?
1. Mistake: Handing in a basic CE mark as proof of quality during a Tier 1 mining tender.
2. Consequence: The mine owner will throw the equipment right off the site. A generic CE certificate only validates basic electrical safety. It doesn’t prove the HDPE pipe fusion machine maintains perfect alignment or accurately records weld data.
3. How to Avoid It: Make sure you procure an HDPE pipe welding machine with data logger capabilities, and demand the specific ISO 12176 certification designed explicitly for plastic pipe welding accuracy.
Step-by-Step Supplier Selection Process and Final Recommendation
A disciplined procurement process guarantees contractors get compliant, rugged fusion equipment on time and on budget. By laying out precise technical needs, issuing standardized RFQs, and running factory audits, procurement teams can confidently choose a supplier ready to tackle the extreme demands of South American mining.
Step 1 to Step 7: From Project Requirements to Pre-Shipment Inspection
1. Define Parameters: Pinpoint the exact pipe OD range, the site altitude, and the SDR rating.
2. Standardize RFQ: Send a highly detailed Request for Quotation to 3 to 5 vetted manufacturers.
3. Evaluate Compliance: Run quotes through a weighted scorecard to gauge ISO compliance and technical depth.
4. Technical Clarification: Set up engineering meetings to iron out data logger specs, frequency, and voltage.
5. Factory Audit: Demand a live video walkthrough of the factory and ask to see a sample weld test in real-time.
6. Negotiate Terms: Lock in the contract, paying special attention to operator training, warranty scope, and the spare parts package.
7. Pre-Shipment Inspection: Require a fully documented Factory Acceptance Test (FAT) before the supplier crates the equipment for ocean freight.
What to Include in Your RFQ to Get Comparable Quotes
Vague RFQs lead to vague pricing. Be hyper-specific. List the exact pipe diameters, the maximum wall thickness (SDR), the site’s electrical frequency and voltage, and the required welding standard (DVS or ASTM). Above all, state clearly that an integrated data logger is mandatory, and ask for a line-item price on a critical spare parts package.
Final Recommendation for Mining Contractors in Chile, Peru, Brazil, and Beyond
Mining contractors working across South America must value traceability and absolute reliability over upfront capital savings. You need CNC or data-logger-equipped hydraulic butt fusion welding machines featuring robust hydraulic seals and proven temperature stability. Partnering with a factory-direct manufacturer that truly understands high-altitude derating and handles export logistics seamlessly will protect your project timeline and guarantee decades of leak-free pipeline performance.
—
FAQ
Q1: What size HDPE pipe fusion machine is needed for mining tailings pipelines?
Because tailings lines pump highly abrasive materials, they use large-diameter, extremely thick-walled HDPE pipes. Contractors usually need heavy-duty hydraulic butt fusion machines ranging from 800mm up to 1200mm or larger. The hydraulic cylinders on these units must be powerful enough to overcome the massive drag pressure of SDR 9 or SDR 7.4 pipes.
Q2: Does high altitude affect HDPE butt fusion welding parameters and generator performance?
Absolutely. Once you pass 3,000 meters in elevation, thinner air causes diesel generators to suffer severe power derating, meaning contractors must heavily oversize their kVA capacity. On top of that, high winds and freezing ambient temperatures pull heat away from the heater plate. You’ll often need protective welding shelters just to keep fusion temperatures stable.
Q3: How much does a large-diameter HDPE pipe butt fusion machine cost?
Pricing swings wildly depending on the automation level, included accessories, and maximum diameter. A basic 630mm hydraulic unit costs a fraction of a fully CNC automatic butt fusion machine outfitted with electric cranes and data loggers. Don’t forget to factor in import duties and ocean freight to find your true landed cost.
Q4: Is electrofusion or butt fusion better for HDPE pipes on mining sites?
For long pipeline runs, hydraulic butt fusion takes the crown due to its incredible joint strength and capacity for handling thick-wall, large-diameter pipes. Electrofusion certainly has its place, but crews generally save it for tight trenches, complex tie-ins, and emergency repairs where a bulky hydraulic carriage won’t fit.
Q5: How long does it take to ship an HDPE pipe fusion machine from China to Chile or Peru?
Ocean freight from major Chinese ports (like Shanghai) takes about 28 to 38 days to reach Callao, Peru, and 32 to 42 days to hit San Antonio, Chile. Keep in mind, you also need to budget 20 to 45 days for the factory to actually build large-diameter or customized CNC automatic butt fusion machines.
Q6: What standards should an HDPE pipe butt fusion machine meet for mining tenders?
Most mining tenders demand ISO 12176-1 for mechanical accuracy and ISO 12176-4 for data logging and traceability. Depending on the exact project specs, the HDPE pipe jointing machine must also execute welds that meet DVS 2207-1 (low pressure), ASTM F2620 (high pressure), or ISO 21307 parameters.
Q7: Can one HDPE pipe fusion machine handle multiple pipe diameters and SDR ratings?
Yes. Hydraulic butt fusion machines use interchangeable liner clamps (reduction inserts) so a single chassis can weld several smaller pipe sizes. Just remember that the butt fusion welding machine’s core hydraulic system still needs enough power to handle the thickest SDR rating of its maximum rated pipe diameter.
Q8: Should mining contractors buy or rent HDPE pipe fusion machines?
If you’re managing multiple pipeline packages or working on long-term projects, buying factory-direct equipment delivers a far better return on investment. Renting makes sense for short-term emergency repairs or highly specialized, one-off large-diameter tie-ins where buying a brand new butt fusion welding machine doesn’t make financial sense.
—
Conclusion
Choosing the right HDPE pipe fusion machine isn’t just a box to check—it’s a foundational move that dictates the safety, timeline, and profitability of your entire South American mining pipeline project. Thick-walled tailings pipes, aggressive temperature swings, and extreme high-altitude environments require heavy-duty, high-pressure hydraulic equipment. Procurement teams have to look past basic price tags and aggressively verify technical specs, from proper high-altitude generator sizing to heater plate temperature stability and hydraulic gauge accuracy.
Meeting the uncompromising QA/QC expectations of mine owners is equally critical. Deploying butt fusion welding machines equipped with advanced data loggers that satisfy ISO 21307 and ISO 12176 standards provides digital traceability for every single weld, shielding contractors from massive liabilities and rework costs. By demanding strict factory acceptance tests, locking down a critical spare parts package upfront, and using a weighted evaluation scorecard, contractors can effectively neutralize the logistical risks of remote site operations. In the end, partnering with a technically proficient supplier who truly understands the brutal realities of the Andean mining sector will secure your project’s success and guarantee decades of pipeline integrity.
Let our experts help you choose the right equipment for your project
Contact Our Engineering Team